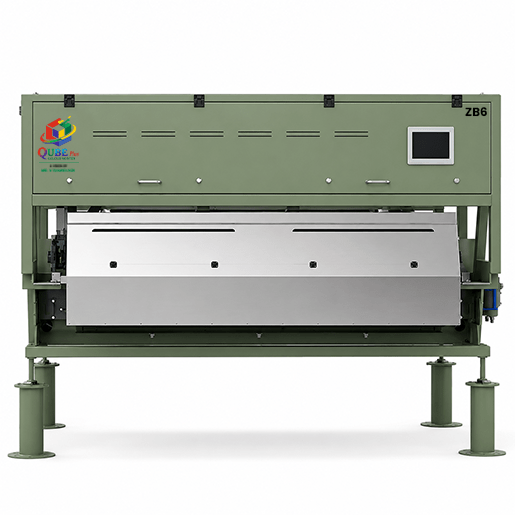
ZB6
₹249.00
High-Resolution Imaging
Equipped with a high-performance 5400-pixel RGB CCD camera, the ZB6 delivers exceptional image clarity and precise color detection for highly accurate and consistent sorting. Advanced imaging technology enables reliable identification of subtle color variations, ensuring superior product quality and enhanced sorting efficiency.
Advanced LED Illumination
Utilizes a high-reliability, long-life LED illumination system that provides uniform and stable lighting for enhanced image clarity and accurate color recognition. Its durable design ensures consistent performance over extended operating periods while minimizing maintenance requirements.
Smart Software System
Powered by intelligent sorting algorithms and a user-friendly software interface, the ZB6 enables efficient operation, precise sorting, and easy system configuration. Flexible calibration settings allow operators to quickly adjust the machine according to specific color standards and diverse processing requirements.
Remote Support Capabilities
Enables advanced remote diagnostics, debugging, and maintenance support for faster troubleshooting and efficient technical assistance. This helps reduce equipment downtime, improve service response, and maintain smooth and uninterrupted sorting operations.
Food-Grade Conveyor Belt
Features a high-quality food-grade PVC conveyor belt designed for safe, hygienic, and smooth material handling. The durable conveyor system ensures reliable product movement while supporting the demanding requirements of modern food processing environments.
Ideal for compact and mid-sized processing facilities, the ZB6 Color Sorting Machine combines cutting-edge sorting technology, durable construction, and a space-efficient design to deliver reliable long-term performance and value. Its advanced capabilities help improve productivity, reduce material waste, maintain consistent product quality, and maximize overall operational efficiency.
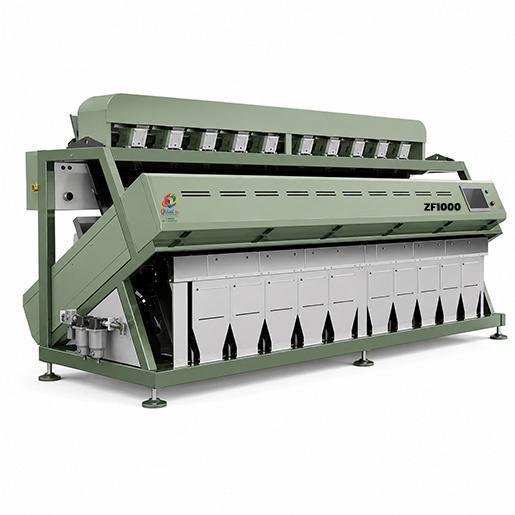
ZF1000
₹249.00
High-Resolution Imaging
Equipped with a 5400-pixel RGB CCD camera for precise color detection and accurate sorting.
Advanced LED Illumination
High-reliability, long-life LED lighting enhances image clarity and ensures consistent, long-lasting performance.
Smart Software System
Efficient and stable software with intelligent algorithms and a user-friendly interface enables easy calibration according to specific color standards.
Remote Support Capabilities
Supports remote debugging, diagnostics, and maintenance, helping reduce downtime and improve service efficiency
Reliable Bulk Processing
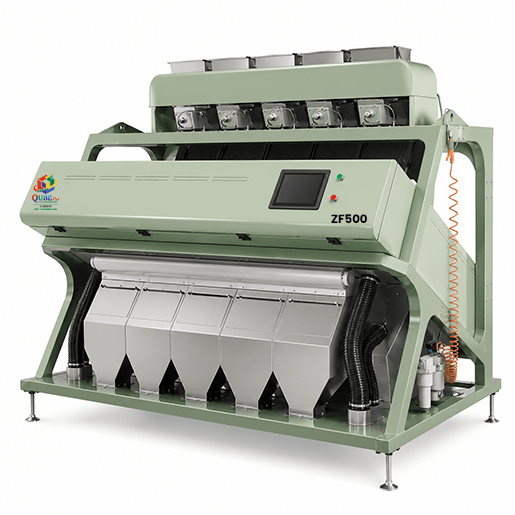
Designed for modern bulk processing operations, the ZF1000 combines advanced technology with a robust design to deliver consistent performance, long-term productivity, and profitability.
ZF1000
₹249.00
High-Resolution Imaging: Equipped with a 5400-pixel RGB CCD camera for precise colour detection and accurate sorting performance.
Advanced LED Illumination: A high-reliability, long-life LED light source enhances image clarity while supporting consistent performance and extended operational longevity.
Smart Software System: Efficient and stable software, powered by intelligent algorithms and a user-friendly interface, enables easy calibration to specific colour standards.
Remote Support Capabilities: Remote debugging, diagnostics, and maintenance help minimize downtime and improve overall service efficiency.
Designed for modern bulk processing operations, the ZF1000 combines advanced technology with a robust design to deliver reliable long-term productivity and profitability.
Contact us today to learn more or request a demo and discover how the ZF1000 can support your sorting operations.
ZF1000
₹249.00
High-Resolution Imaging
Equipped with a 5400-pixel RGB CCD camera for precise color detection, exceptional image clarity, and highly accurate sorting performance.
Advanced LED Illumination
Features a high-reliability, long-life LED light source that enhances image clarity, provides consistent illumination, and supports reliable operation over extended periods.
Smart Software System
Powered by efficient and stable software, intelligent algorithms, and a user-friendly interface, enabling precise sorting and easy calibration according to specific color standards.
Remote Support Capabilities
Enables remote debugging, diagnostics, and maintenance support, helping reduce operational downtime, accelerate troubleshooting, and improve overall service efficiency.
ZF1000
₹249.00
High-Resolution Imaging
Equipped with a 5400-pixel RGB CCD camera, the ZF1000 delivers precise color recognition, exceptional image clarity, and highly accurate sorting for consistent product quality.
Advanced LED Illumination
A high-reliability, long-life LED lighting system provides uniform illumination, enhancing image detection, sorting accuracy, and long-term operational stability.
Intelligent Software System
Powered by advanced sorting algorithms and a stable, user-friendly interface, the ZF1000 enables quick calibration and precise adjustment to specific color standards for efficient and consistent sorting.
Remote Support & Diagnostics
Integrated remote debugging, diagnostics, and maintenance capabilities help minimize downtime, simplify troubleshooting, and ensure reliable processing performance.
Built for Productivity & Profitability
Designed for modern bulk processing operations, the ZF1000 combines cutting-edge sorting technology with a robust, durable design to deliver high productivity, consistent quality, optimized efficiency, and long-term profitability.